Manufacturing Excellence
Manufacturing Quality Medicines with Precision and Care
At SK pharma Ltd (Salah Kakar Pharmaceutical Company), manufacturing is the foundation of our commitment to improving healthcare. Every pharmaceutical product we produce is the result of carefully designed processes, modern technology, skilled professionals, and rigorous quality systems that work together to ensure safety, efficacy, and consistency.

From raw material receipt to the release of finished products, every manufacturing activity is conducted under controlled conditions, supported by documented procedures, qualified personnel, and validated systems that ensure consistent product quality.
Our manufacturing facility has been established to support the production of high-quality pharmaceutical products while meeting the requirements of GMP rules and the expectations of healthcare professionals, patients, and regulatory authorities.
Our Manufacturing Philosophy
We believe that pharmaceutical manufacturing is more than a production process—it is a responsibility to patients.
Every tablet, capsule, and oral liquid manufactured by SK pharma is produced with the understanding that it may directly improve or protect someone’s health. Therefore, quality is integrated into every stage of our manufacturing operations rather than being inspected only at the end.
Our philosophy is based on five key principles:
- Patient safety comes first.
- Quality is everyone’s responsibility.
- Continuous improvement drives operational excellence.
- Innovation strengthens manufacturing performance.
- Compliance builds trust.
Through this approach, we continuously improve our manufacturing systems while maintaining strict compliance with pharmaceutical regulations and quality standards.
Modern Manufacturing Facility
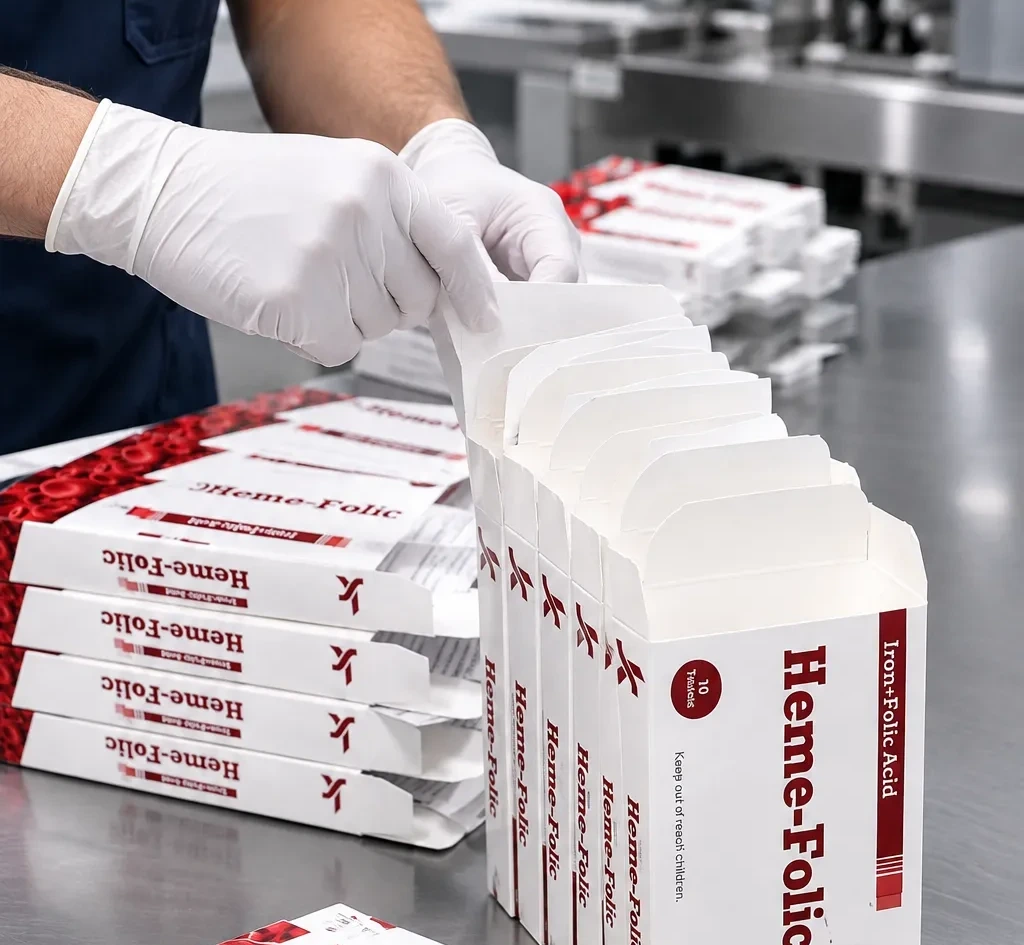
Our production facility has been designed to provide an efficient, hygienic, and well-controlled environment for pharmaceutical manufacturing.
The facility layout promotes a logical flow of personnel, materials, and products, minimizing the risk of cross-contamination while supporting efficient manufacturing operations.
Dedicated production areas, environmental controls, and carefully maintained equipment ensure that every manufacturing process is performed under appropriate conditions.
The facility includes:
Warehouse Management
Effective warehouse management is essential to maintaining pharmaceutical quality.
Our warehouse operations are organized to ensure:
Raw Material Storage
Incoming raw materials are received, inspected, quarantined, sampled, tested, approved, and stored under appropriate environmental conditions before use.
Packaging Material Storage
Packaging materials are segregated and managed according to approved inventory control procedures.
Finished Goods Storage
Released finished products are stored under specified environmental conditions until distribution.
Warehouse operations follow the principles of:
- First Expiry First Out (FEFO)
- First In First Out (FIFO)
- Environmental monitoring
- Inventory traceability
- Controlled access
Utilities Supporting Manufacturing
Reliable utility systems are essential for maintaining pharmaceutical manufacturing quality.
Our utility systems include:
HVAC System
HVAC systems control temperature, humidity, pressure, airflow, air cleanliness, ventilation rate, and air circulation in enclosed spaces.
Purified Water System
Purified water is produced, monitored, and distributed through a validated system designed to meet pharmaceutical quality requirements.
Compressed Air System
Oil-free compressed air is supplied to manufacturing equipment where required and is routinely monitored to ensure quality.
Electrical Systems
Reliable electrical infrastructure and backup power systems support uninterrupted manufacturing operations
Environmental Monitoring
Critical manufacturing areas are routinely monitored to verify compliance with established environmental standards.
Engineering and Maintenance
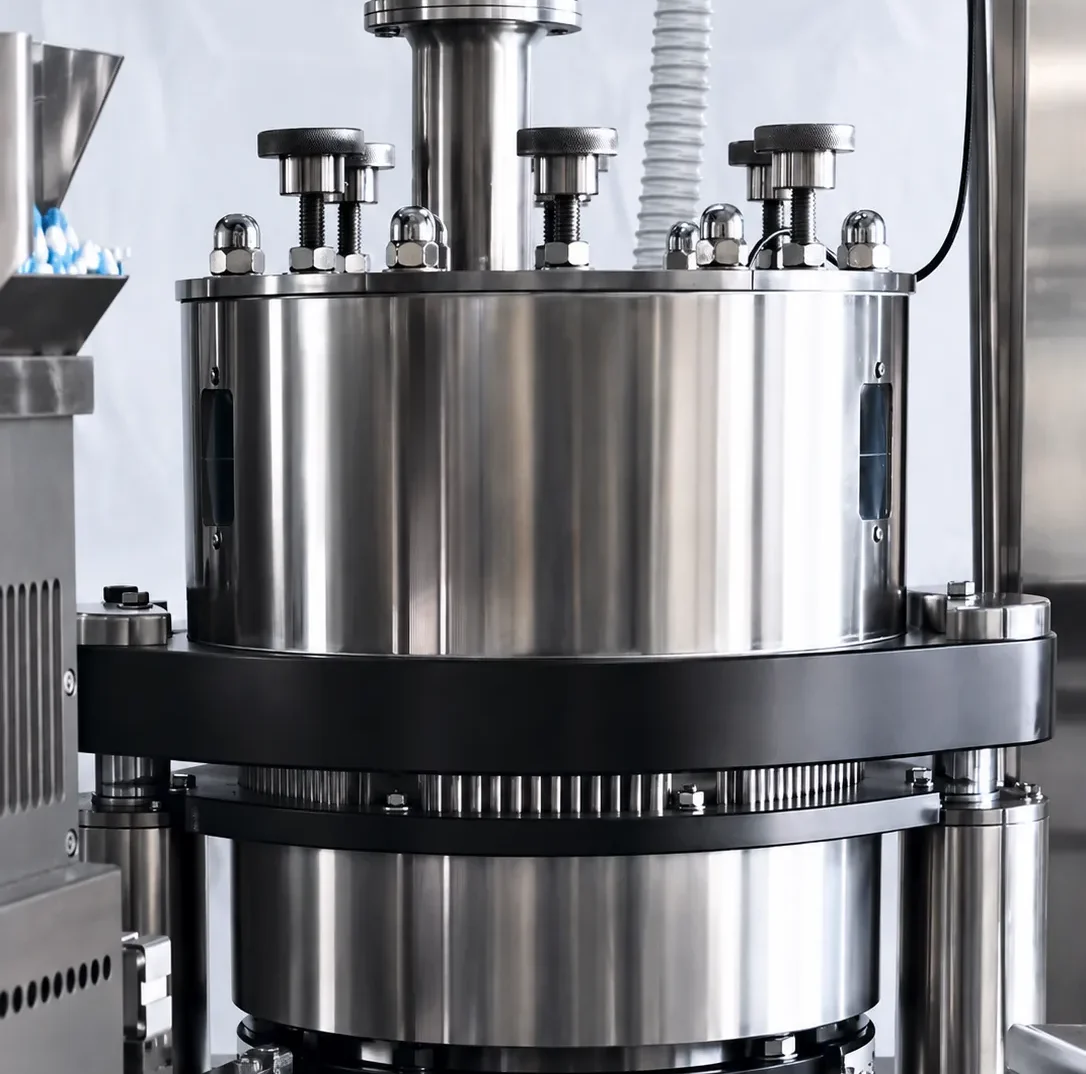
Our engineering department supports manufacturing through preventive maintenance, equipment qualification, calibration, utilities management, and continuous technical improvement.
Engineering activities include:
Well-maintained equipment contributes directly to product quality, manufacturing efficiency, and operational reliability.
Manufacturing Workflow
Every product manufactured at SK pharma follows a structured and documented process to ensure consistency and compliance.
Good Manufacturing Practices (GMP)
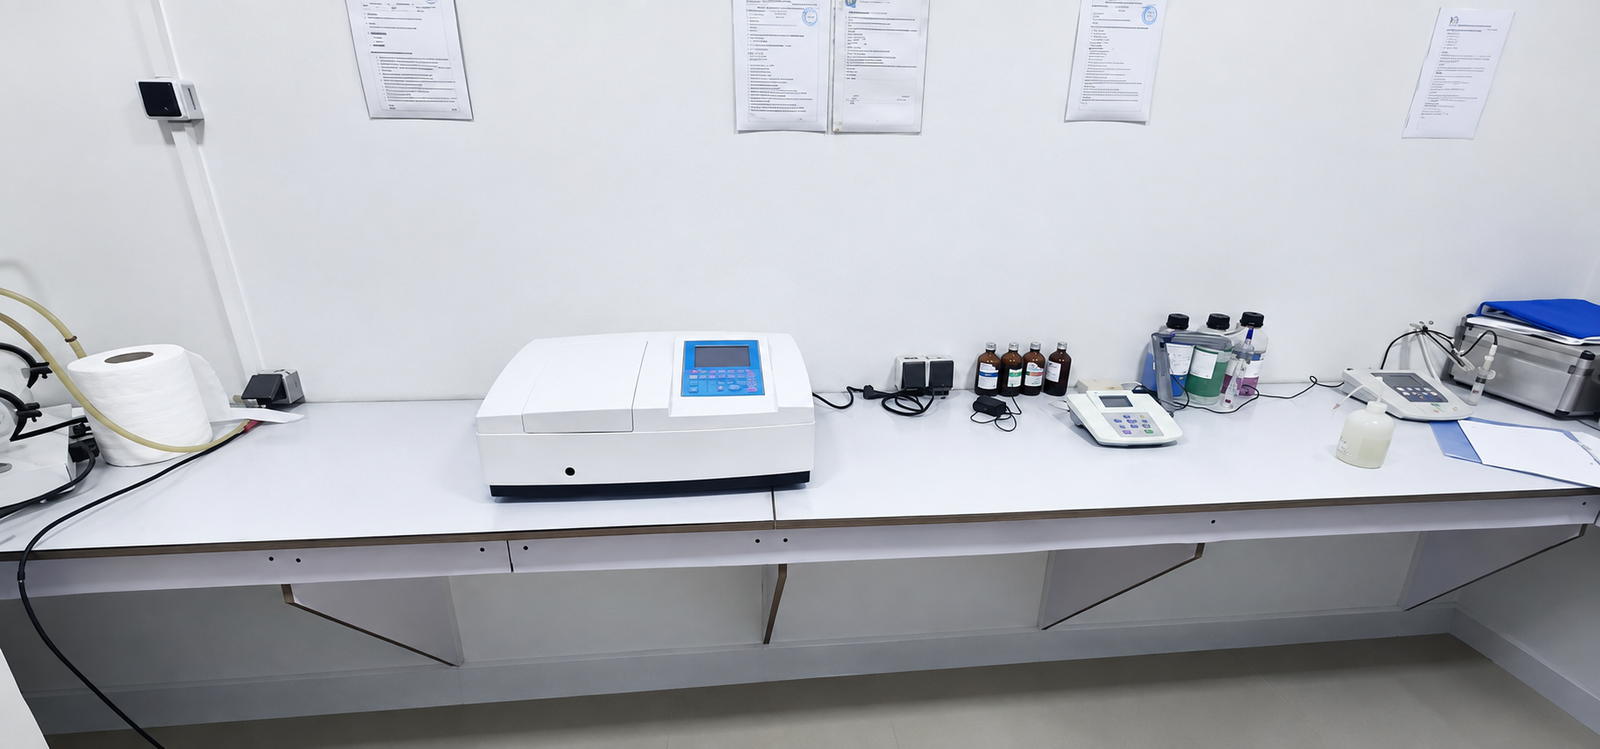
Quality is embedded in every aspect of our manufacturing operations through adherence to GMP rules
Our manufacturing systems emphasize:
Commitment to Continuous Improvement
The pharmaceutical industry is constantly evolving, and so are we.
SK pharma continuously evaluates new technologies, manufacturing practices, and quality systems to improve productivity, efficiency, sustainability, and product quality.
We encourage innovation throughout the organization while maintaining our commitment to regulatory compliance and patient safety.
Through investment in people, technology, and infrastructure, we are building a manufacturing organization capable of meeting future healthcare challenges.
Manufacturing for a Healthier Tomorrow
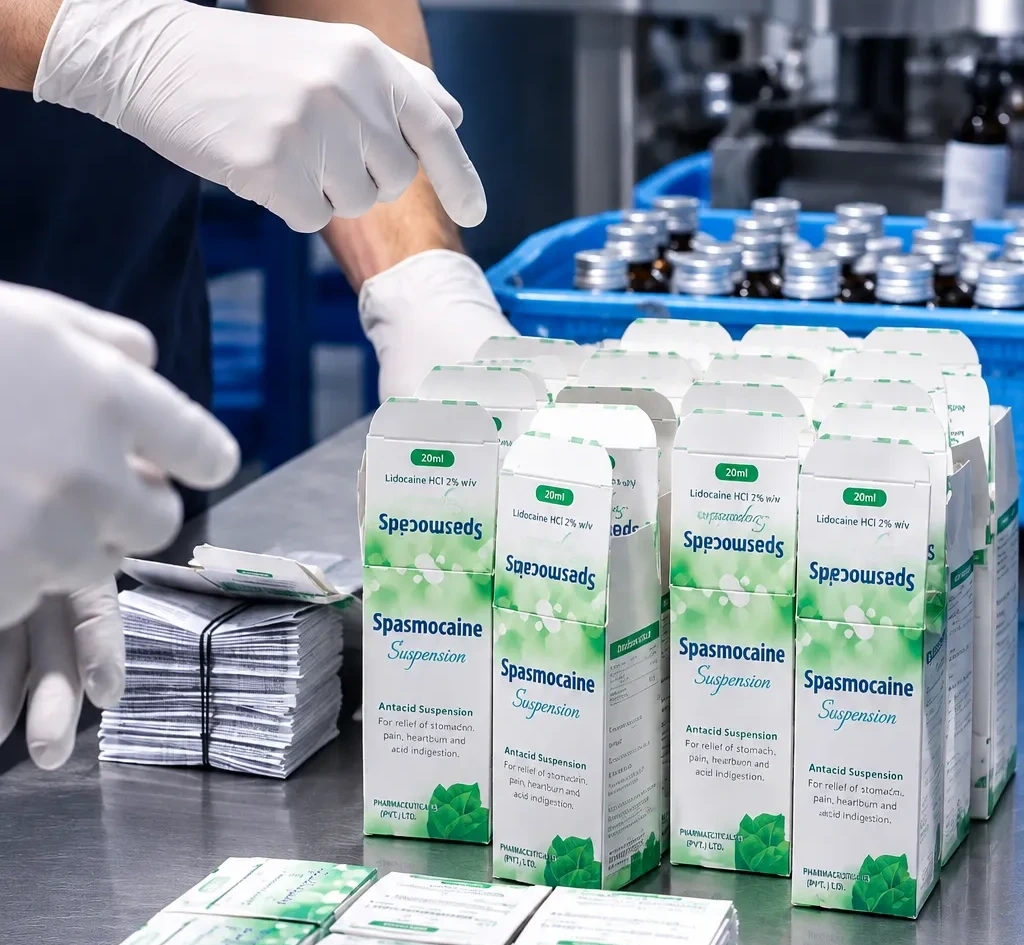
Every product that leaves our manufacturing facility represents our commitment to quality, responsibility, and care.
By combining scientific knowledge, advanced manufacturing technologies, skilled professionals, and comprehensive quality systems, SK pharma is helping improve access to safe, effective, and affordable medicines for patients across Afghanistan.
As we continue to expand our capabilities, we remain dedicated to manufacturing excellence and to supporting the health and well-being of the communities we serve.